How to Choose the Right Cap Mold for Your Business?
Choosing the right Cap Mold can determine whether your production line runs smoothly or struggles with waste, delays, and inconsistent quality. The mold shapes the closure, affects sealing performance, and influences how customers perceive your packaging. A suitable choice must match your bottle neck size, resin type, production speed, and filling environment. It should also support stable cooling, easy demolding, and repeatable dimensions.
Experience shows that a mold performing well in one factory may fail in another. Machine pressure, cooling water temperature, and operator skills can change the result. Even a small mismatch may create flash, uneven threads, or loose caps. These defects are easy to notice during inspection. They are harder to correct after thousands of pieces are produced.
Before selecting a Cap Mold, review your product drawings and test samples with a qualified mold supplier. Ask about steel grade, cavity layout, maintenance access, expected service life, and replacement parts. Reliable suppliers should explain their testing process rather than promise unrealistic results. Production trials are valuable, but they are not perfect. Materials change, equipment ages, and early assumptions may prove wrong. Leave room for adjustment.
This guide explores practical factors for choosing a Cap Mold that fits your current needs and future plans. It also considers cost, quality control, delivery reliability, and technical support. The cheapest option may not be the most economical choice. A well-designed mold can reduce downtime, protect product consistency, and support steady business growth.
Classify Cap Molds by Closure Type, Neck Finish, Cavities, and Material
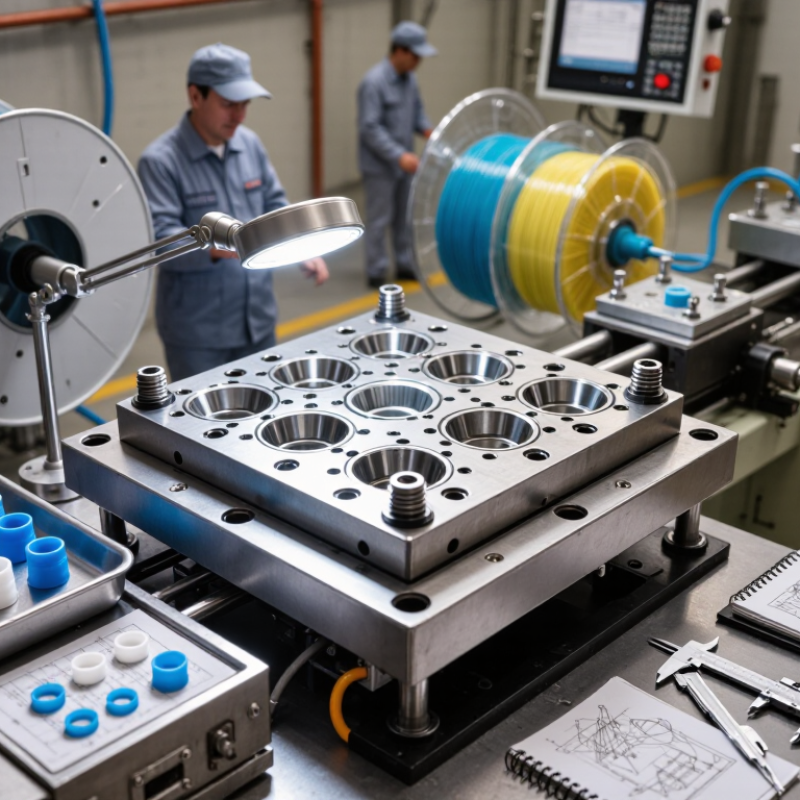
Choosing the right cap mold starts with the closure type. Screw caps need accurate thread geometry and stable torque control. Snap-on caps require precise locking rings and balanced ejection. Sport or dispensing closures often demand moving cores, seals, and tighter alignment. The neck finish must match the cap exactly. Small differences in thread pitch, bead height, or opening diameter can cause leakage. Industry standards such as ISBT 18806 help define lightweight plastic neck finishes, but real bottle performance still requires physical testing.
Cavities determine output, maintenance, and risk. A 48-cavity mold can produce high volumes, yet poor cooling may create uneven shrinkage across the layout. According to Grand View Research, the global plastic caps and closures market was valued at approximately USD 73 billion in 2023. That scale increases pressure for faster, more consistent molding. Material selection matters too. Hardened tool steel supports long production runs, while corrosion-resistant steel suits demanding environments. PlasticsEurope reported global plastics production at 400.3 million tonnes in 2022, showing the importance of efficient material use. I have seen teams choose more cavities too early. It looked efficient, but maintenance became slower. Mold decisions should consider resin behavior, cycle time, cleaning access, and actual order volume—not only the machine’s maximum capacity.
How to Choose the Right Cap Mold for Your Business
Compare common packaging neck finishes by nominal diameter. Use the finish specification—not diameter alone—to confirm cap and bottle compatibility.
Choosing a mold: First match the closure type and neck finish, including thread and sealing details. Then select cavity count to suit required output and machine capacity. Finally, confirm the cap resin—commonly PP or HDPE—is appropriate for the product and use conditions.
The diameters shown are nominal finish designations in millimeters, not complete finish dimensions. Verify the applicable finish drawing and tolerances before tooling; cavity count and mold material depend on the production requirements.
Match Mold Design with 28 mm, 38 mm, and Other Industry Standards
Choosing a cap mold starts with the bottle neck, not the cap alone. A 28 mm PCO finish suits many carbonated beverage containers, while 38 mm finishes support wider openings and higher product flow. The dimensions are not interchangeable. Thread pitch, neck height, tamper-band clearance, and sealing surface must match the target standard precisely.
Industry data supports careful specification. PlasticsEurope reported that packaging represented about 39.5% of European plastics demand in 2021. This makes lightweighting important, but thinner caps demand tighter mold control. The PMMI Beverage Packaging Trends report also identifies lightweighting and recyclability as major packaging priorities. A mold with poor cooling can create uneven walls, ovality, or weak bands. Small defects become expensive when cavity counts increase.
During mold trials, measure torque, leakage, bridge strength, and removal force across every cavity. For 28 mm caps, even slight thread mismatch can cause leaks under carbonation pressure. For 38 mm closures, check panel flatness and sealing performance around the larger opening. Material shrinkage also changes with resin grade and cycle temperature. A mold may pass the first trial, yet fail after continuous production. That is the uncomfortable part. Design reviews should include actual neck samples, not only drawings. Citeable standards and plant measurements matter more than attractive computer images.
How to Choose the Right Cap Mold for Your Business? - Match Mold Design with 28 mm, 38 mm, and Other Industry Standards
Use the package’s specified neck-finish drawing to select a compatible cap design. Nominal diameter alone does not establish thread, sealing, or tamper-evidence compatibility.
| Nominal Size |
Common Finish or Closure Family |
Typical Packaging Applications |
Cap Mold Design Considerations |
Checks Before Production |
| 28 mm |
PCO 1881 beverage finish |
Carbonated soft drinks, water, and other beverage bottles designed for this finish |
Match the thread profile, sealing surface, and tamper-evident band geometry to the specified PCO finish. Confirm that the cap design suits the product’s pressure and sealing requirements. |
Verify the bottle-finish drawing, cap application and removal requirements, pressure performance, and tamper-band separation. |
| 28 mm |
PCO 1810 beverage finish |
Beverage bottles using the PCO 1810 neck finish |
Do not assume it is interchangeable with PCO 1881 because both are nominally 28 mm. Design the mold around the exact thread and finish specification. |
Confirm the finish designation with the bottle supplier and test fit, seal integrity, and opening performance on production bottles. |
| 28 mm |
28/410 continuous-thread finish |
Personal-care, household, and some liquid-product containers |
Match the cap’s thread and liner or sealing feature to the container. If the closure includes a dispensing insert or orifice, account for its fit and assembly in the design. |
Check the neck-finish drawing, closure function, seal method, and compatibility with the intended liquid. |
| 38 mm |
38 mm continuous-thread finish |
Food jars and other containers specified for a 38 mm threaded closure |
Specify the exact thread profile and finish rather than relying on diameter. Allow for the selected liner or sealing feature and ensure the cap engages without excessive application torque. |
Validate thread engagement, seal performance, application torque, removal torque, and package fit. |
| 45 mm |
45 mm continuous-thread finish |
Wide-mouth food and household containers using a matching threaded finish |
Design the thread, top panel, and sealing surface to the container specification. Check wall and panel design for the intended closure material and molding process. |
Confirm the finish drawing, closure-to-container fit, sealing method, and performance after filling and storage. |
| 63 mm |
63 mm lug or threaded closure family, as specified |
Food jars and other wide-mouth containers designed for the selected closure system |
Lug and continuous-thread systems are different designs. Match the cap’s engagement features to the container finish and the required sealing process. |
Identify the exact finish and closure type; test engagement, seal integrity, opening behavior, and any process-specific requirements. |
Estimate Output Using Cavity Count, Cycle Time, and Scrap Rate
How to Choose the Right Cap Mold for Your Business?
Estimate practical output before selecting a cap mold. Cavity count shows how many parts form during one cycle. Cycle time determines how often that mold repeats production. Use this basic calculation: cavities × 3,600 ÷ cycle seconds. An eight-cavity mold running an 18-second cycle produces about 1,600 caps per hour before losses. Real production is lower. Cooling delays, material changes, maintenance, and operator adjustments reduce available time.
Apply uptime and scrap rate to create a more reliable estimate. If the line operates at 85% uptime and scrap reaches 3%, the result becomes about 1,319 usable caps hourly. This figure is more valuable than a perfect theoretical number. Check cap weight, thread accuracy, sealing performance, and ejection stability during trials. I have seen molds with impressive cavity counts lose output because cooling was uneven. More cavities are not always better. A neat spreadsheet can still lie.
Tips: Record actual cycle times from several shifts, not one test run. Measure scrap by cause, including flash, short shots, and damaged threads. Leave capacity for cleaning and mold servicing. Ask whether your equipment can maintain balanced filling across every cavity. If the mold runs too aggressively, quality problems may quietly erase the expected profit. Recheck the estimate after production begins. Forecasts improve when factory data replaces assumptions.
Evaluate ±0.05 mm Tolerances, Cooling Design, Maintenance, and Total Cost
Choosing a cap mold starts with dimensional risk, not the lowest quotation.
A ±0.05 mm tolerance can affect thread fit, seal compression, and automated capping. ISO 20457 provides guidance for molded plastic part tolerances, but real performance depends on resin shrinkage, steel stability, and machine control. Ask for inspection records from trial production. Check cavity-to-cavity variation, not only one approved sample. Small detail. A mold may pass initial inspection and drift after thousands of cycles.
Cooling design deserves equal attention.
Balanced channels should remove heat evenly around every cavity, especially near threads and sealing surfaces. PlasticsEurope’s Plastics—The Fast Facts 2023 reports 400.3 million tonnes of plastics production in 2022. That scale increases pressure for shorter cycles and stable output. The International Energy Agency’s Energy Efficiency 2023 report states that industry used about 37% of global final energy in 2022. Efficient cooling can therefore influence both cycle time and operating cost. Still, I would not assume more channels always mean better cooling. Poor layouts can create weld lines, warpage, or difficult maintenance.
Calculate total cost across the mold’s expected life.
Include spare inserts, polishing, water treatment, inspection time, rejected caps, and planned downtime. For example, a 0.5-second cycle reduction can create substantial annual capacity when multiplied across many cavities and shifts. Maintenance access matters too. Quick-change components may cost more initially but reduce lost production. Request a maintenance schedule, cooling-flow test, and cavity replacement estimate. The uncomfortable question remains: is the ±0.05 mm requirement genuinely necessary for your closure design? Over-specification can increase cost without improving customer performance.